Shree Krishna Exports
India’s Trusted Rice Export Company
Certified Long-grain basmati rice exporters by ISO 22000:2005 and ISO 9001:2015
We continuously strive to drive innovation in the rice industry through dedicated research and the development of premium-quality & cost-effective solution.”
With decades of industry expertise, Shree Krishna Exports has earned a solid reputation as a leading Indian company engaged in the production, processing and export of both basmati and non-basmati rice. With over 23 years of consistent presence, we possess in-depth market knowledge and operational excellence. Our business practices are rooted in integrity, transparency and professionalism at each level. We are one of the Leading Basmati Rice Mannufacturers & Suppliers in Haryana, India.
Why “Shree Krishna Exports”?
Ensuring Purity and Perfection
Expert Team
Our team comprises skilled professionals who bring creativity and innovation to their respective fields. They seamlessly integrate deep-rooted traditional knowledge with modern expertise and advanced technologies to enhance both pre- and post-harvesting practices. With a strong focus on quality, they follow strict hygiene protocols at every stage—from production to packaging. Our experienced team collaborates efficiently to ensure smooth and well-organized operations across the organization. Each product undergoes thorough inspection, ensuring that only the finest quality reaches our customers.
Our Facilities / Infrastructure
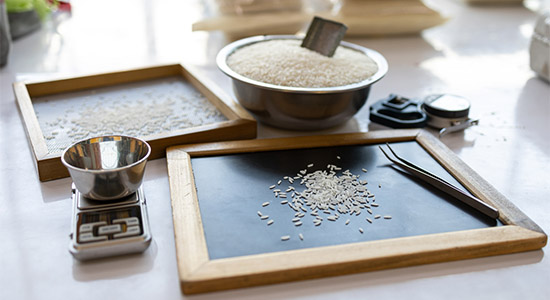
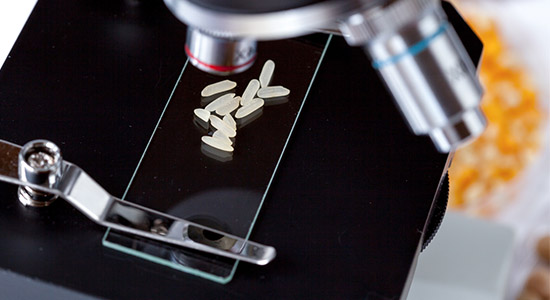
Our advanced and state-of-the-art, high-technology rice processing facility consistently delivers food grains that meet the highest standards of quality, safety, and hygiene. A fully equipped laboratory rigorously tests all raw materials, packaging components, in-process parameters, and finished products to ensure uncompromised quality output. The entire facility is modernized, with upgraded machinery for grain conditioning, storage, and treatment processes. The drying plant, integrated with sensor-based technology, ensures precise and continuous drying while effectively preserving the grain’s natural aroma.
Quality Is Paramount
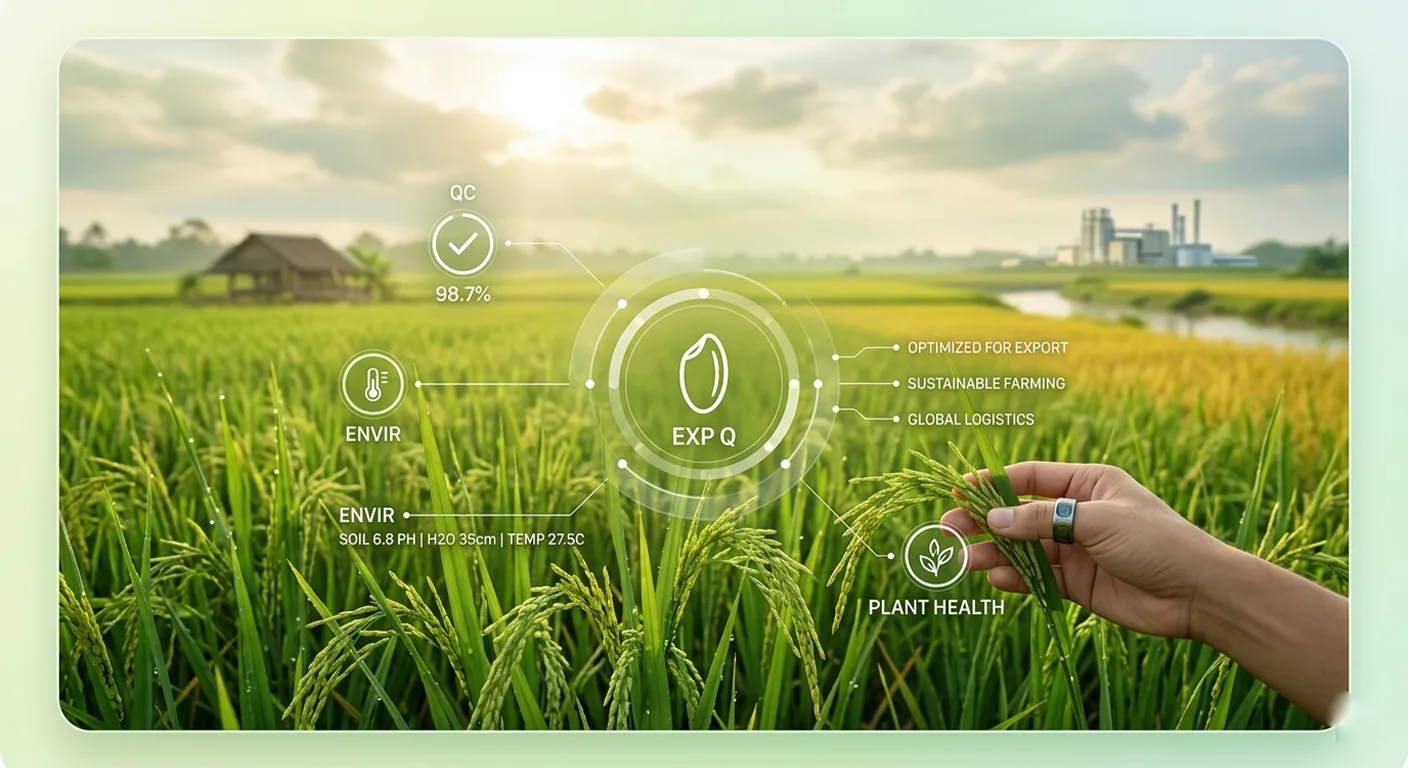
As one of India’s leading exporters of basmati rice, we follow the finest organic cultivation, harvesting and processing practices. Our ISO-certified range undergoes stringent quality checks at every stage—from cultivation and harvesting to milling, storage and final packaging. Each batch of raw and processed basmati rice is thoroughly tested in our APEDA-approved laboratory to ensure superior quality and consistency.
Entering the Global Marketplace
Our core exports include pesticide-free organic rice, premium basmati rice, and high-quality non-basmati rice. We deliver our products across India and international markets through a well-established network of key dealers, distributors and retailers. Our major global presence spans Europe, the USA, Canada, Saudi Arabia, Bahrain, Qatar, Kuwait, Oman, Yemen, Jordan, Egypt, Turkey, Israel, Lebanon, Iraq, Erbil, Australia, New Zealand, and Mauritius. We are known for superior quality, lasting freshness, and extended shelf life, our products are consistently trusted and appreciated by customers worldwide.
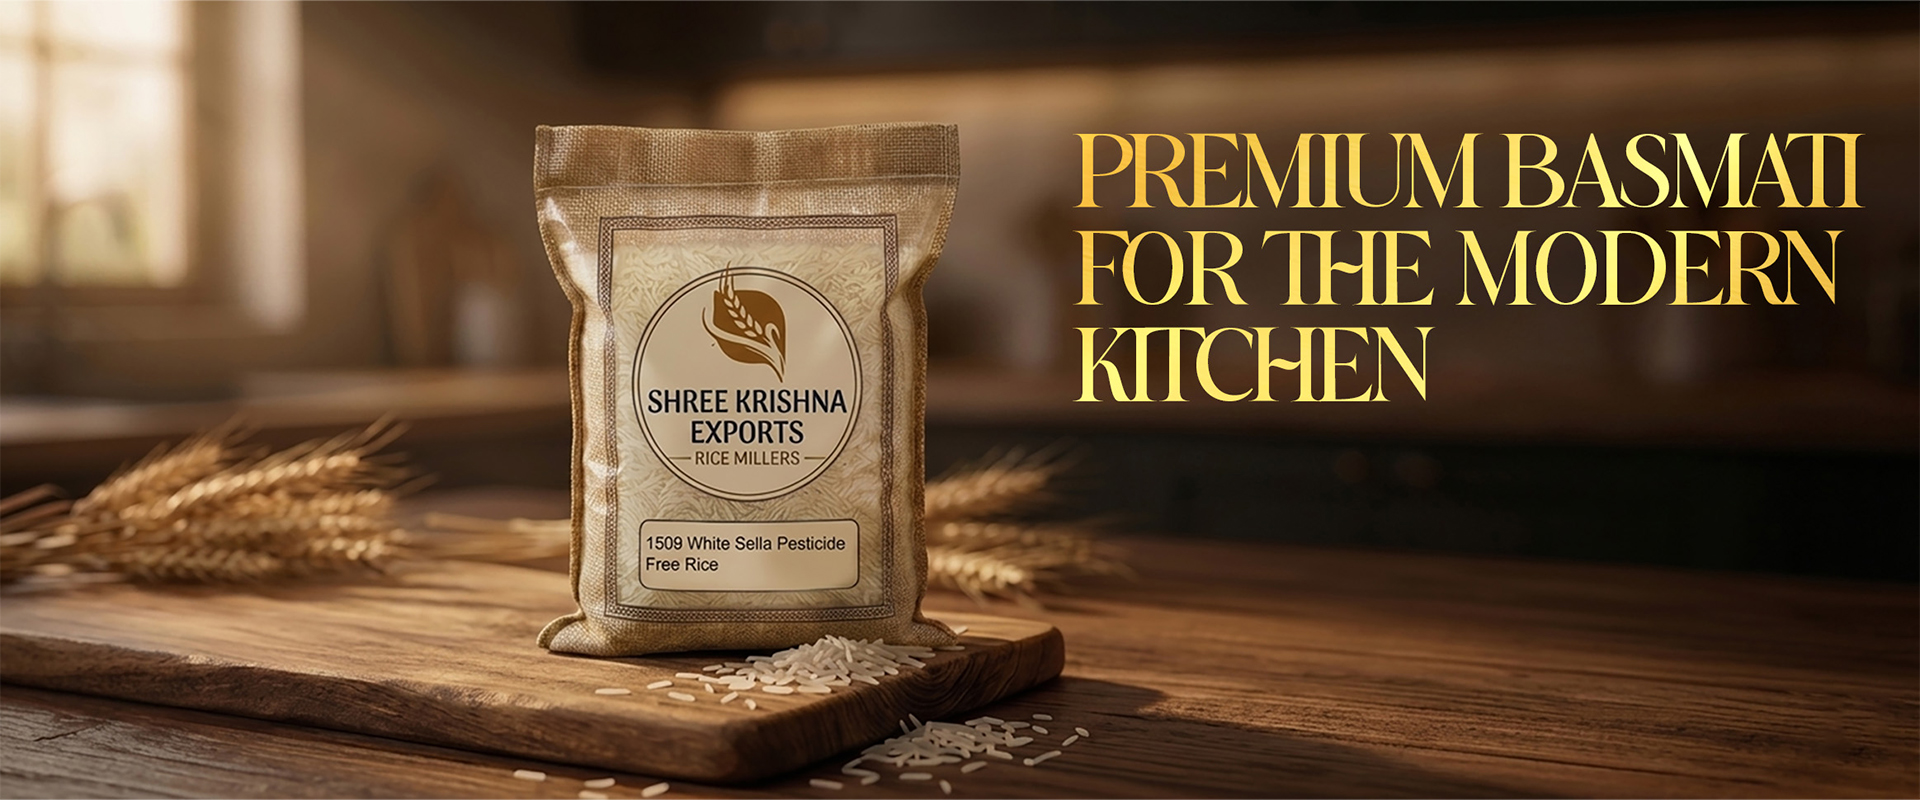
Shree Krishna Exports is one of the trusted Basmati Rice Manufacturers, Suppliers, and Exporter in India, offering Grade-A quality 1121, 1509, 1401, 1718, and Traditional Basmati Rice. Our rice is known for its long grains, rich aroma, excellent taste, and non-sticky texture after cooking. we are also Leading Basmati Rice Manufacturers & suppliers in Haryana. With advanced milling, strict quality checks, and hygienic packaging, we ensure consistent quality for domestic and international markets. We provide bulk basmati rice supply at competitive prices to wholesalers, distributors, hotels, and food businesses. We are among the leading Basmati Rice Manufacturers and Suppliers in Haryana, offering high-quality basmati rice for bulk orders, wholesalers, distributors, and exporters.
Looking for High-Quality Basmati Rice Manufacturers ? Contact Shree Krishna Exports today for bulk orders, competitive prices, and reliable supply solutions!
Expert Team
Our team comprises skilled professionals who bring creativity and innovation to their respective fields. They seamlessly integrate deep-rooted traditional knowledge with modern expertise and advanced technologies to enhance both pre- and post-harvesting practices. With a strong focus on quality, they follow strict hygiene protocols at every stage—from production to packaging. Our experienced team collaborates efficiently to ensure smooth and well-organized operations across the organization. Each product undergoes thorough inspection, ensuring that only the finest quality reaches our customers.
Why “Shree Krishna Exports”?
Ensuring Purity and Perfection
Entering the Global Marketplace
Our core exports include pesticide-free organic rice, premium basmati rice, and high-quality non-basmati rice. We deliver our products across India and international markets through a well-established network of key dealers, distributors and retailers. Our major global presence spans Europe, the USA, Canada, Saudi Arabia, Bahrain, Qatar, Kuwait, Oman, Yemen, Jordan, Egypt, Turkey, Israel, Lebanon, Iraq, Erbil, Australia, New Zealand, and Mauritius. We are known for superior quality, lasting freshness, and extended shelf life, our products are consistently trusted and appreciated by customers worldwide.
Quality Is Paramount
As one of India’s leading exporters of basmati rice, we follow the finest organic cultivation, harvesting and processing practices. Our ISO-certified range undergoes stringent quality checks at every stage—from cultivation and harvesting to milling, storage and final packaging. Each batch of raw and processed basmati rice is thoroughly tested in our APEDA-approved laboratory to ensure superior quality and consistency.
Our Facilities / Infrastructure
Our advanced and state-of-the-art, high-technology rice processing facility consistently delivers food grains that meet the highest standards of quality, safety, and hygiene. A fully equipped laboratory rigorously tests all raw materials, packaging components, in-process parameters, and finished products to ensure uncompromised quality output. The entire facility is modernized, with upgraded machinery for grain conditioning, storage, and treatment processes. The drying plant, integrated with sensor-based technology, ensures precise and continuous drying while effectively preserving the grain’s natural aroma.